Additive Manufacturing Metrology: Verifying Parts That Fail in Ways Machined Parts Don’t
Additive manufacturing creates geometries, internal structures and process-related variations that can be difficult to verify using conventional inspection alone. Metrology provides the measurement data needed to understand whether a printed part actually matches its intended design.
In This Article
- Why additive manufacturing needs a different inspection approach
- Common dimensional and geometric failure modes
- CAD comparison and full-field inspection
- Surface quality and complex geometry
- Internal defects, porosity and hidden structures
- CMM vs 3D scanning vs industrial CT
- Process validation and first article inspection
- ZEISS metrology solutions for additive manufacturing
Additive manufacturing changes the relationship between design, manufacturing and inspection.
Instead of removing material from a larger block or forming a component around a mould, the part is constructed layer by layer according to a digital manufacturing process.
That approach makes highly complex geometries possible, including lightweight structures, internal channels, lattice structures and consolidated assemblies. But the same freedom introduces failure modes that may not be obvious from the outside of the finished component.
A printed part can appear visually correct while still containing dimensional deviations, deformation, surface variation, porosity or internal features that do not match the intended design.
This is why additive manufacturing metrology needs to look beyond simple pass-or-fail dimensional checks.
Why Additive Manufacturing Needs a Different Inspection Approach
Conventional machined parts generally begin with a known block, blank or preform from which material is removed. Inspection can therefore focus heavily on defined dimensions, datums, holes, surfaces and geometric relationships.
Additive manufacturing introduces another variable: the build process itself can influence the final geometry and material structure.
Build orientation, thermal effects, support structures, layer deposition, powder behaviour, heat treatment and part removal can all influence the final component.
The inspection question is therefore not only “Is the part the right size?” It is also: “Did the manufacturing process produce the geometry, surface and internal structure that the design requires?”
- Dimensional accuracy
- Geometric deviation
- Warpage and distortion
- Surface quality
- Internal porosity
- Voids and defects
- Internal channels
- CAD-to-part deviation
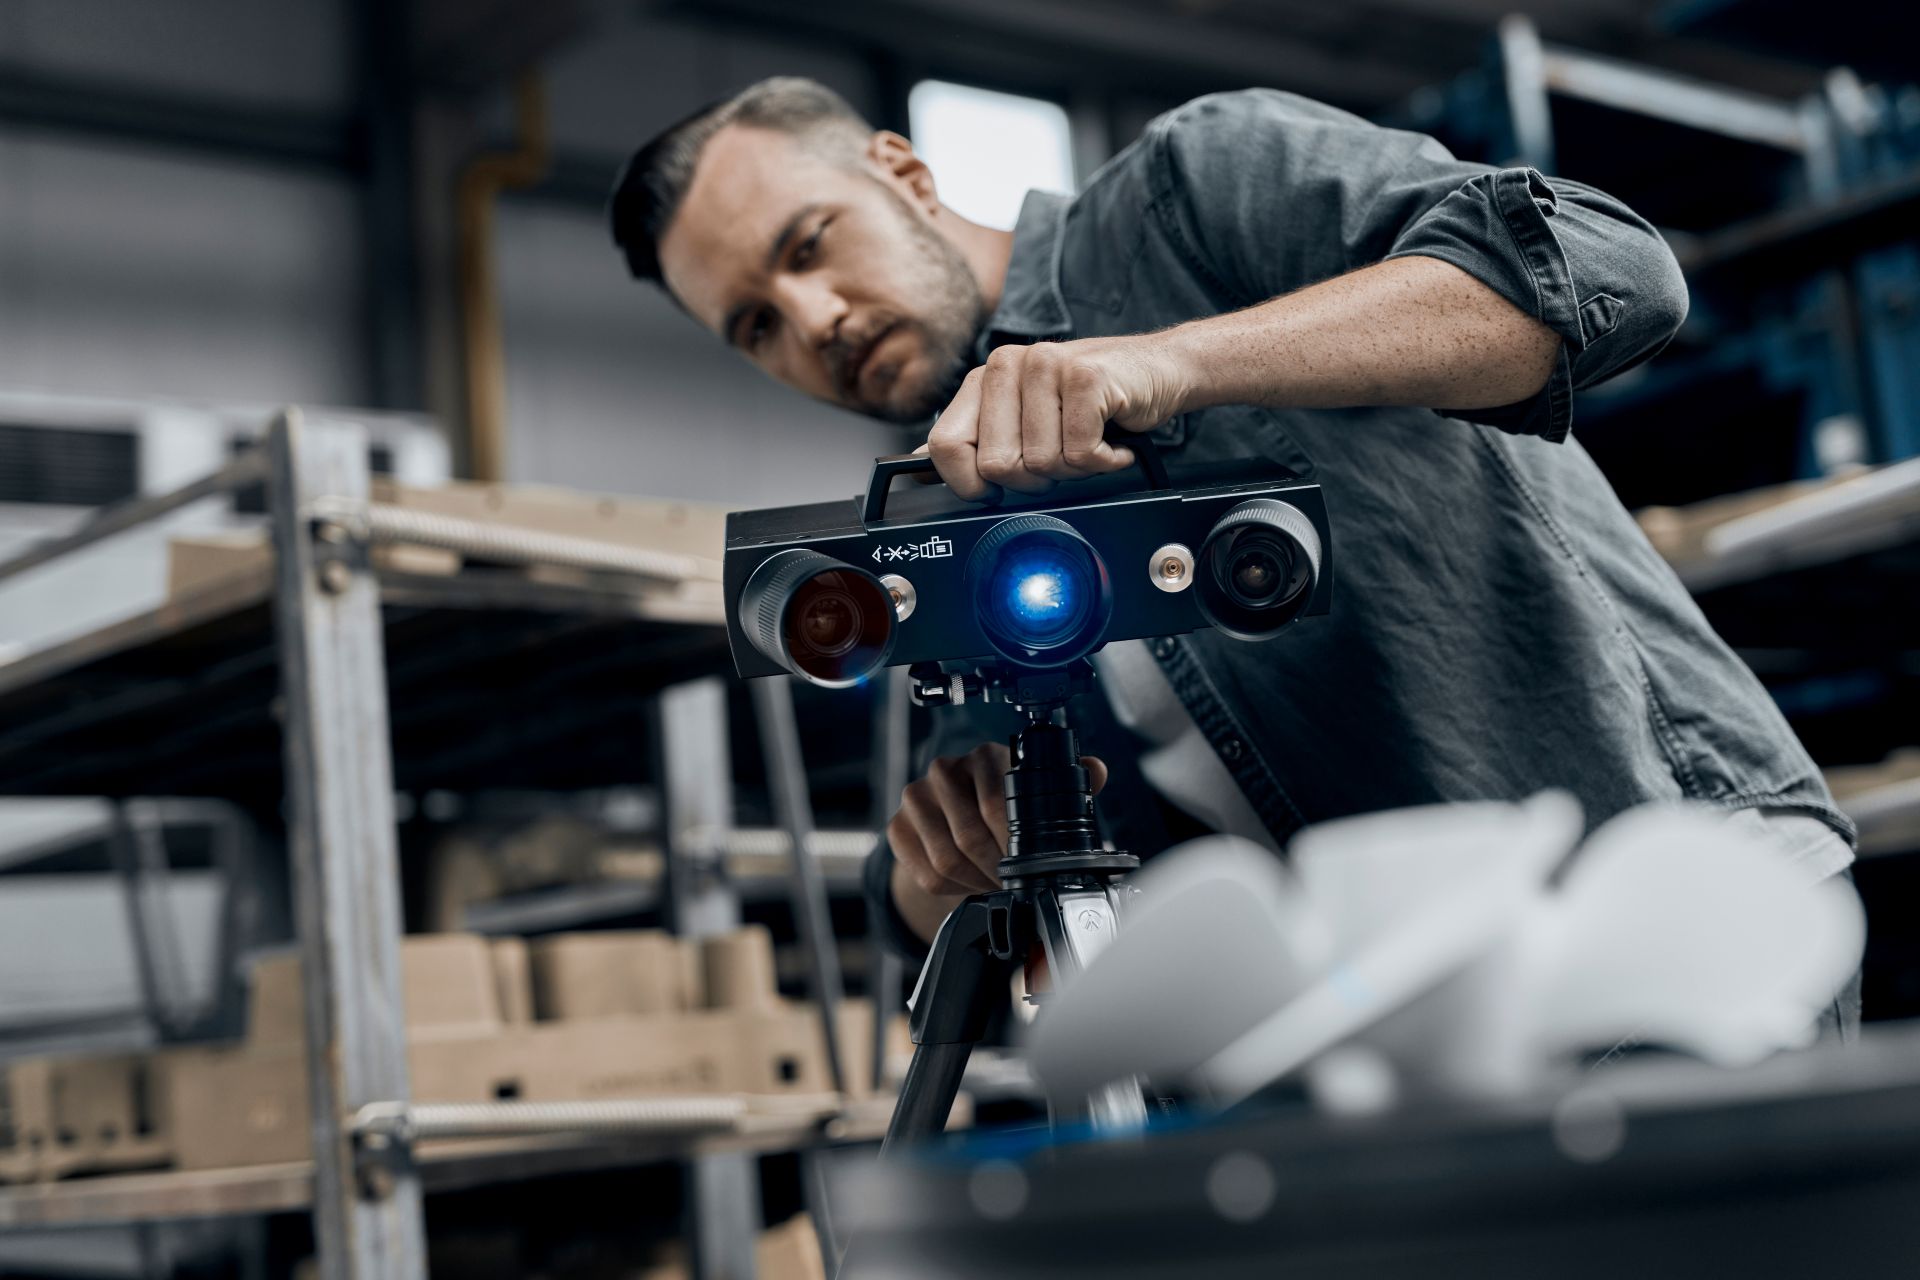
What Can Go Wrong With an Additively Manufactured Part?
Additive manufacturing defects can appear at different stages of production. Some can be detected on the external surface, while others only become apparent when the finished component is compared with CAD or inspected internally.
Warpage and Distortion
Thermal effects and residual stresses can cause a component to deform during or after the build. A part may remain recognisable while no longer matching the intended geometry.
Dimensional Deviation
Critical holes, mounting interfaces, walls and other features can shift from their nominal positions and require verification against engineering requirements.
Surface Variation
Layer-based production produces surface characteristics that differ from conventional machining. Optical measurement can capture the resulting surface geometry across the component.
Porosity and Voids
Internal defects can form within the printed structure without producing an obvious external indication. Industrial CT can provide non-destructive visibility into these regions.
Internal Features
Internal channels, cavities and lattice structures can be difficult or impossible to inspect using external measurement alone.
Post-Processing Effects
Heat treatment, support removal, machining and other finishing operations can alter the final geometry of a printed part.
Dimensional Inspection of Additively Manufactured Parts
Dimensional inspection remains fundamental to additive manufacturing. The difference is that a printed component can contain considerably more complex and freeform geometry than a conventional machined part.
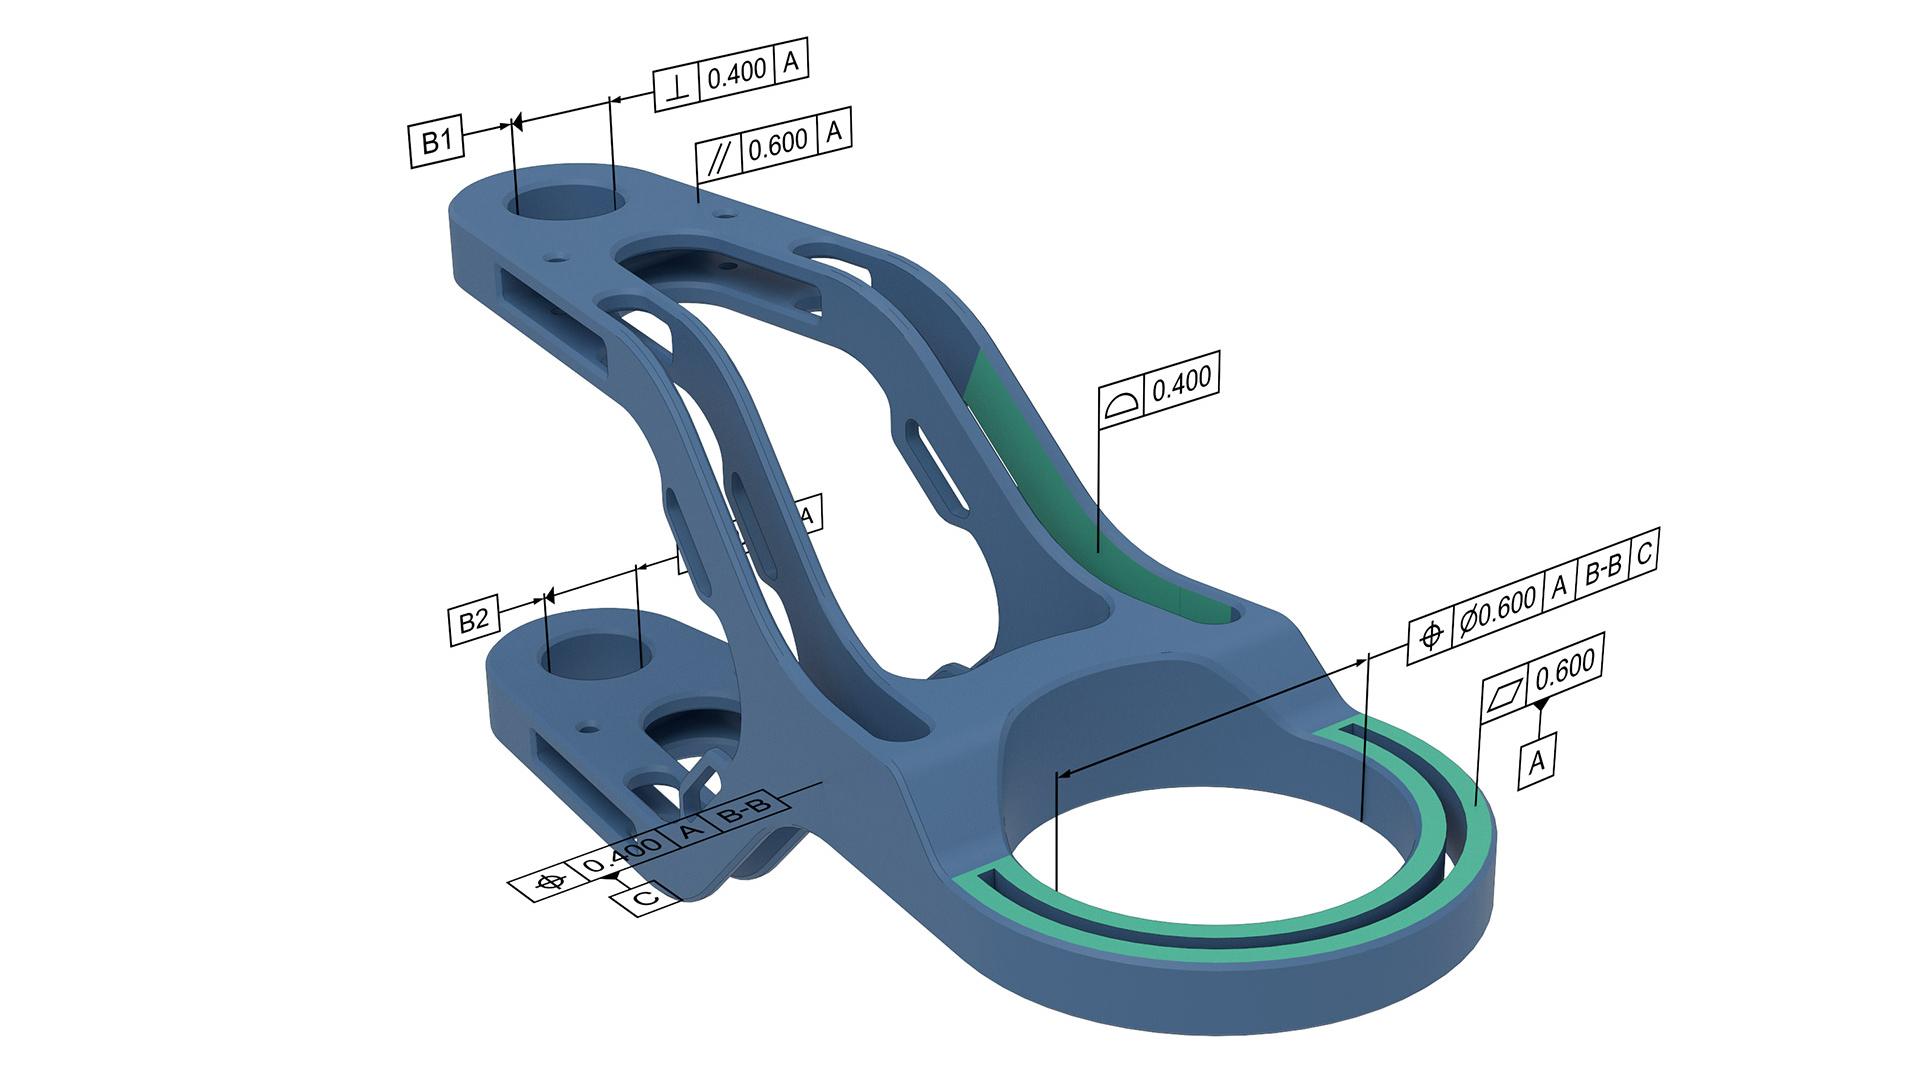
Critical characteristics can include hole diameters, feature positions, wall thicknesses, mounting interfaces, overall envelope dimensions and geometric tolerances.
For components with clearly defined engineering features, a coordinate measuring machine can provide repeatable measurement of dimensions and geometric relationships.
For components dominated by complex freeform surfaces, optical 3D scanning can capture substantially more surface information, allowing deviations to be visualised across the complete part.
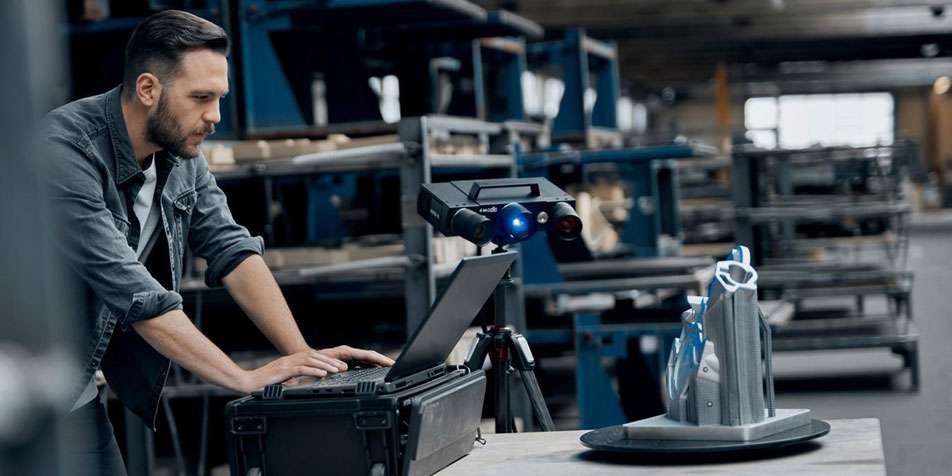
Part-to-CAD Comparison: Seeing Where the Printed Part Deviated
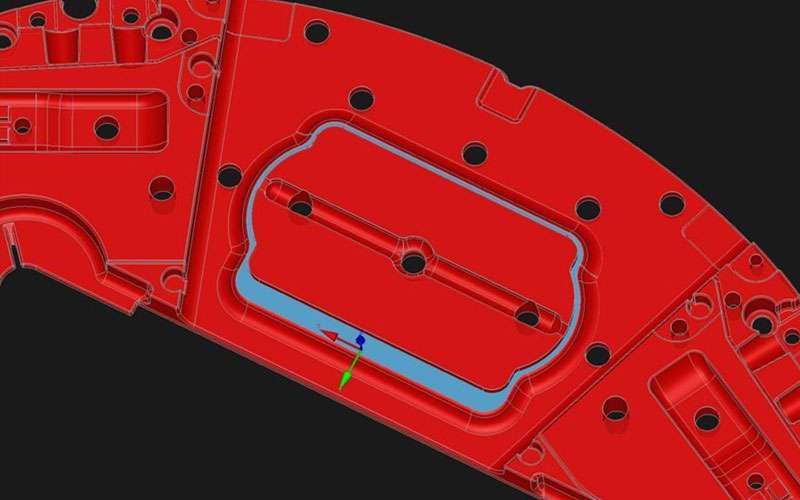
One of the most useful applications of optical 3D metrology in additive manufacturing is part-to-CAD comparison.
Instead of checking only a limited number of dimensions, the measured surface can be aligned with the nominal CAD model and analysed across the complete component.
This makes it possible to identify patterns of deviation rather than simply recording individual pass-or-fail measurements.
Capture
Capture the printed component using an appropriate optical 3D measurement system.
Align
Align the measured data against the nominal CAD geometry using an appropriate inspection strategy.
Analyse
Identify dimensional deviation, deformation and localised surface variation requiring further investigation.
Surface Quality and Complex Geometry
Surface quality becomes especially important when the component contains freeform geometry, thin structures, lattice features or complex transitions between surfaces.
A limited number of tactile measurement points may not fully describe the behaviour of a complex surface. Optical 3D scanning provides a dense representation of the measured geometry, allowing engineers to evaluate a much larger area of the component at once.
This can be useful during prototype validation, process development, first article inspection and production quality control.
For additive manufacturing, the useful measurement result is often not one number. It is the pattern of deviation across the component and what that pattern says about the manufacturing process.
Internal Defects: What Surface Inspection Cannot See
Optical scanners and tactile CMMs are primarily concerned with accessible geometry. Additive manufacturing, however, can create important features and defects inside the component.
Internal channels, cavities, trapped powder, voids and porosity may have no visible indication on the external surface.
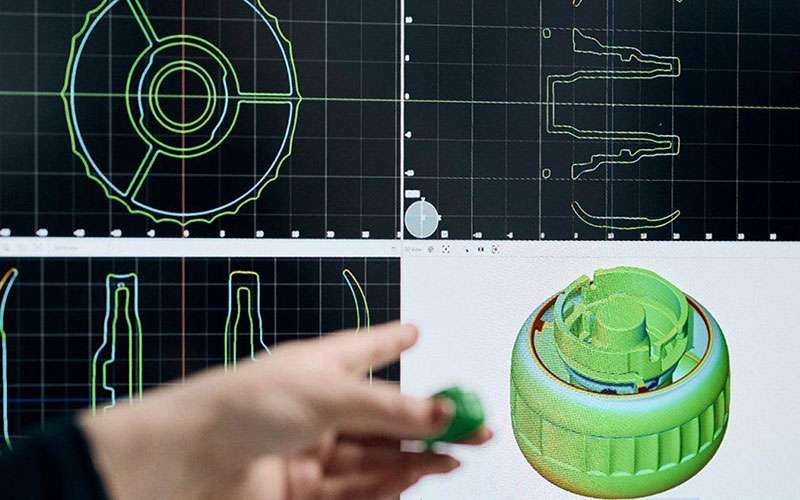
Industrial X-ray computed tomography provides a non-destructive method for reconstructing the internal and external geometry of a component.
This makes CT particularly relevant where the inspection requirement involves hidden geometry, internal defects or structures that cannot be physically accessed by a probe or optical scanner.
CMM vs 3D Scanning vs Industrial CT
No single measurement technology is automatically appropriate for every additive manufacturing inspection task.
The correct approach depends on the geometry, tolerance, accessibility of critical features and whether the inspection needs to cover the surface, the internal structure or both.
| Inspection Requirement | CMM | Optical 3D Scanning | Industrial CT |
|---|---|---|---|
| Defined dimensional features | Strong fit | Suitable depending on geometry | Suitable depending on material and CT requirements |
| Geometric tolerances | Strong fit | Suitable for appropriate features | Suitable for internal and external geometry |
| Complex freeform surfaces | Possible but point-based | Strong fit | Possible through volumetric data |
| Full-field surface measurement | Limited | Strong fit | Possible |
| CAD comparison | Suitable | Strong fit | Suitable |
| Internal channels | Limited by access | Not externally visible | Strong fit |
| Internal porosity and voids | Not normally accessible | Not externally visible | Strong fit |
| Non-destructive internal inspection | Limited | Surface only | Strong fit |
Using Metrology to Understand the Manufacturing Process
Measurement becomes more valuable when it is used to understand why a part changed rather than simply to decide whether a finished part passes inspection.
If several components show a similar deformation pattern, the measurement data can provide evidence that the variation is related to the manufacturing process rather than being an isolated dimensional error.
Comparing parts before and after heat treatment, support removal or other post-processing steps can also help identify when a particular deviation was introduced.
- Compare build-orientation effects
- Identify repeated deformation patterns
- Compare pre- and post-processing geometry
- Identify localised dimensional drift
- Investigate recurring internal defects
- Correlate inspection data with process changes
First Article Inspection for Additive Manufacturing
First Article Inspection is particularly useful when introducing a new additive manufacturing component, changing a production process or qualifying a new manufacturing source.
The objective is to establish whether the manufactured component meets its defined engineering requirements before the process moves into regular production.
Depending on the component, an additive manufacturing first article inspection can combine dimensional measurement, geometric verification, CAD comparison, surface inspection and internal CT inspection.
The inspection method should follow the characteristics that actually matter to the part. A complex printed component may need several complementary measurement technologies rather than one universal inspection method.
ZEISS Metrology Solutions for Additive Manufacturing
Global TechSolutions provides access to ZEISS metrology systems covering optical 3D scanning, coordinate measurement and industrial CT. The appropriate system depends on what the additive manufacturing component needs to be measured.
ZEISS ATOS Q
A compact industrial optical 3D measurement system suited to detailed surface inspection, dimensional analysis and CAD comparison of small to medium-sized components.
Explore ATOS Q →GOM Scan 1
A compact structured-light 3D scanner for dimensional inspection, CAD comparison and detailed 3D data capture of smaller components.
Explore GOM Scan 1 →ZEISS METROTOM 1
Industrial CT provides non-destructive access to internal and external structures, supporting inspection of hidden geometry, defects and complex internal features.
Explore METROTOM 1 →ZEISS METROTOM 800 225kV
Industrial CT for non-destructive inspection of internal structures, defects and dimensional characteristics across suitable precision components and additive manufacturing applications.
Explore METROTOM 800 →ZEISS SPECTRUM
A bridge-type CMM for accurate tactile and optical measurement of defined dimensions, geometric features and production components.
Explore ZEISS SPECTRUM →ZEISS INSPECT
Inspection software for analysing 3D measurement data, supporting workflows such as CAD comparison, dimensional analysis, deviation evaluation and reporting.
Explore ZEISS INSPECT →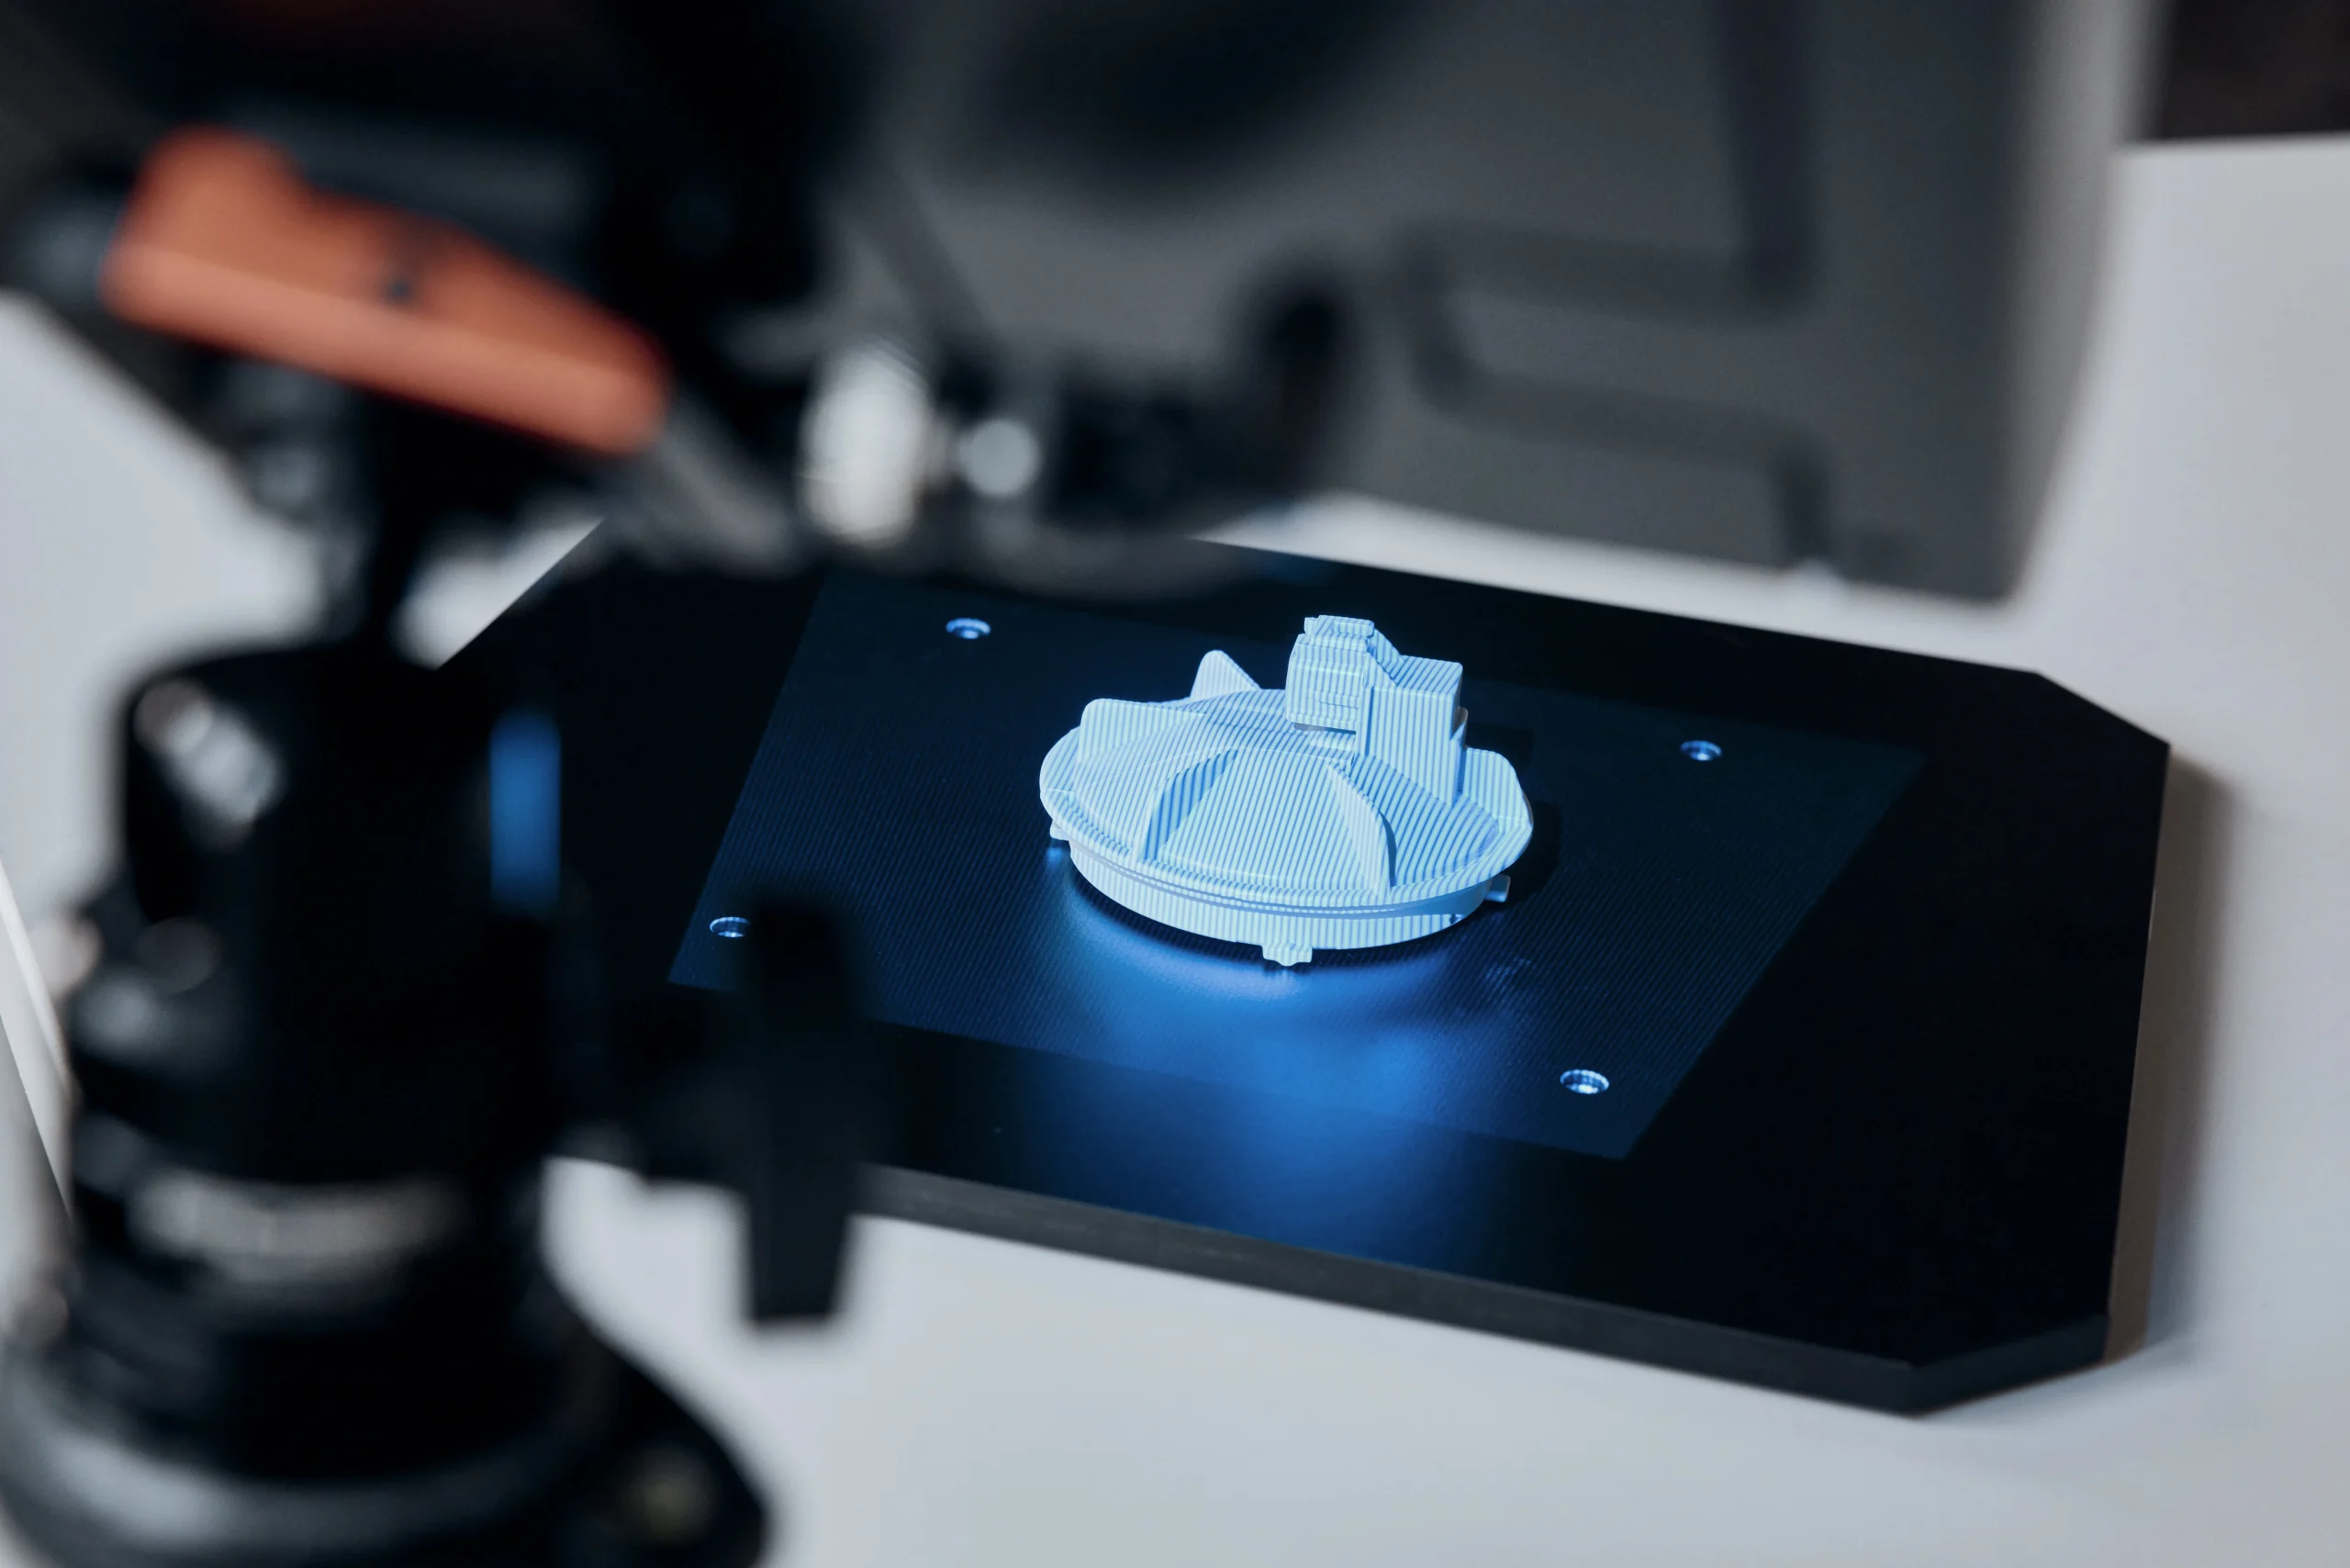
Turning Measurement Data Into an Inspection Result
Capturing a 3D scan or CT dataset is only one stage of the inspection process. The resulting measurement data needs to be aligned, analysed and converted into information that engineers and quality teams can act on.
ZEISS INSPECT supports 3D inspection workflows including CAD comparison, dimensional analysis, deviation evaluation and reporting.
For CMM-based inspection, ZEISS CALYPSO provides measurement workflows for defined geometries and dimensional requirements.
How to Choose the Right Metrology Method
The best inspection approach starts with the component and the engineering question rather than the measurement system.
What Needs to Be Measured?
Identify the critical dimensions, surfaces, interfaces, channels and internal structures that determine whether the component is acceptable.
Are the Critical Features Accessible?
External features may be suitable for CMM or optical inspection. Hidden features may require industrial CT.
Is the Geometry Freeform?
Complex surfaces may benefit from full-field optical 3D scanning and CAD comparison rather than relying only on discrete measurement points.
Do Internal Defects Matter?
If porosity, voids, internal channels or hidden defects are critical, consider whether CT inspection is required.
Is This a One-Off or Recurring Inspection?
Prototype investigation, first article inspection and production inspection can require different measurement workflows and reporting requirements.
What Output Does Engineering Need?
Decide whether the final result needs dimensional reports, CAD deviation maps, defect analysis, wall-thickness data or other inspection documentation.
Why Additive Manufacturing Metrology Matters
Additive manufacturing makes it possible to produce parts that would be difficult, expensive or impossible to manufacture using conventional methods.
That design freedom also means the inspection process needs to understand more than the final external dimensions.
Metrology provides a way to connect the digital design with the physical component.
Optical 3D scanning can show where the surface has deviated from CAD. CMMs can verify defined geometric features and tolerances. Industrial CT can expose internal structures and defects without destroying the part.
Used together where appropriate, these technologies provide a more complete picture of how an additively manufactured component actually turned out.
The important question is not simply how small a measurement system can measure. It is whether the technology can provide the right measurement data for the component, tolerance and manufacturing decision.
Explore Our Metrology Solutions
Download our portfolio to explore our ZEISS industrial metrology solutions, measurement technologies and applications for demanding manufacturing environments.
GTS Metrology Portfolio
Get an overview of our solutions, capabilities and industrial metrology applications.
Download Portfolio ↓Have a part you need to measure?
Bring us your measurement challenge. Discuss your component, tolerance requirements and inspection objectives with our metrology specialists.