Turbine Blade Metrology: Three Zones, Three Methods
A turbine blade is not one measurement problem. Its aerofoil, root attachment and internal cooling passages each present different geometries and inspection challenges, which is why 3D scanning, CMM measurement and industrial CT each have a distinct role in turbine blade inspection.
In This Article
- Why turbine blades require different inspection methods
- 3D scanning for the aerofoil
- CMM measurement for the blade root
- Industrial CT for internal cooling passages
- Turbine blade inspection during MRO
- Reverse engineering worn or legacy blades
- Choosing the right metrology technology
- ZEISS metrology solutions for turbine blades
One Turbine Blade, Three Different Measurement Problems
Turbine blades combine freeform aerodynamic surfaces, tightly controlled attachment features and internal structures that cannot be reached from the outside. Treating the entire component as if it were a single measurement task can therefore make inspection less effective.
The measurement method needs to follow the geometry and the information required from that geometry. For the aerofoil, the objective is often to capture the complete surface and identify deviations against nominal CAD. For the blade root, the focus shifts towards discrete features, datums and geometric tolerances. For internal cooling passages, the challenge is fundamentally different because the geometry is hidden inside the part.
Aerofoil
A complex freeform surface where full-field optical 3D scanning can capture dense surface information for CAD comparison and deviation analysis.
Root Attachment
A set of precisely engineered features where CMM measurement can verify dimensions, form, position and relationships between critical datums and surfaces.
Internal Cooling Passages
Hidden channels and internal walls that require non-destructive inspection technology such as industrial CT to make the internal geometry measurable.
The inspection method should follow the geometry. Freeform surfaces, discrete engineered features and hidden internal structures do not necessarily require the same measurement technology.
The Aerofoil: Why 3D Scanning Fits the Geometry
The aerofoil is the aerodynamic portion of the blade. Its twisted and tapered form creates a continuously changing surface rather than a small collection of simple geometric features.
A tactile CMM can measure an aerofoil, but a point-based approach means the inspection strategy has to determine where individual points or scanning paths should be collected. Optical 3D scanning approaches the problem differently by capturing dense surface information across the blade.
That full-field data can then be compared with nominal CAD geometry. Instead of looking only at isolated measurement points, engineers can examine surface deviations across the blade and identify areas where geometry has shifted from the intended form.
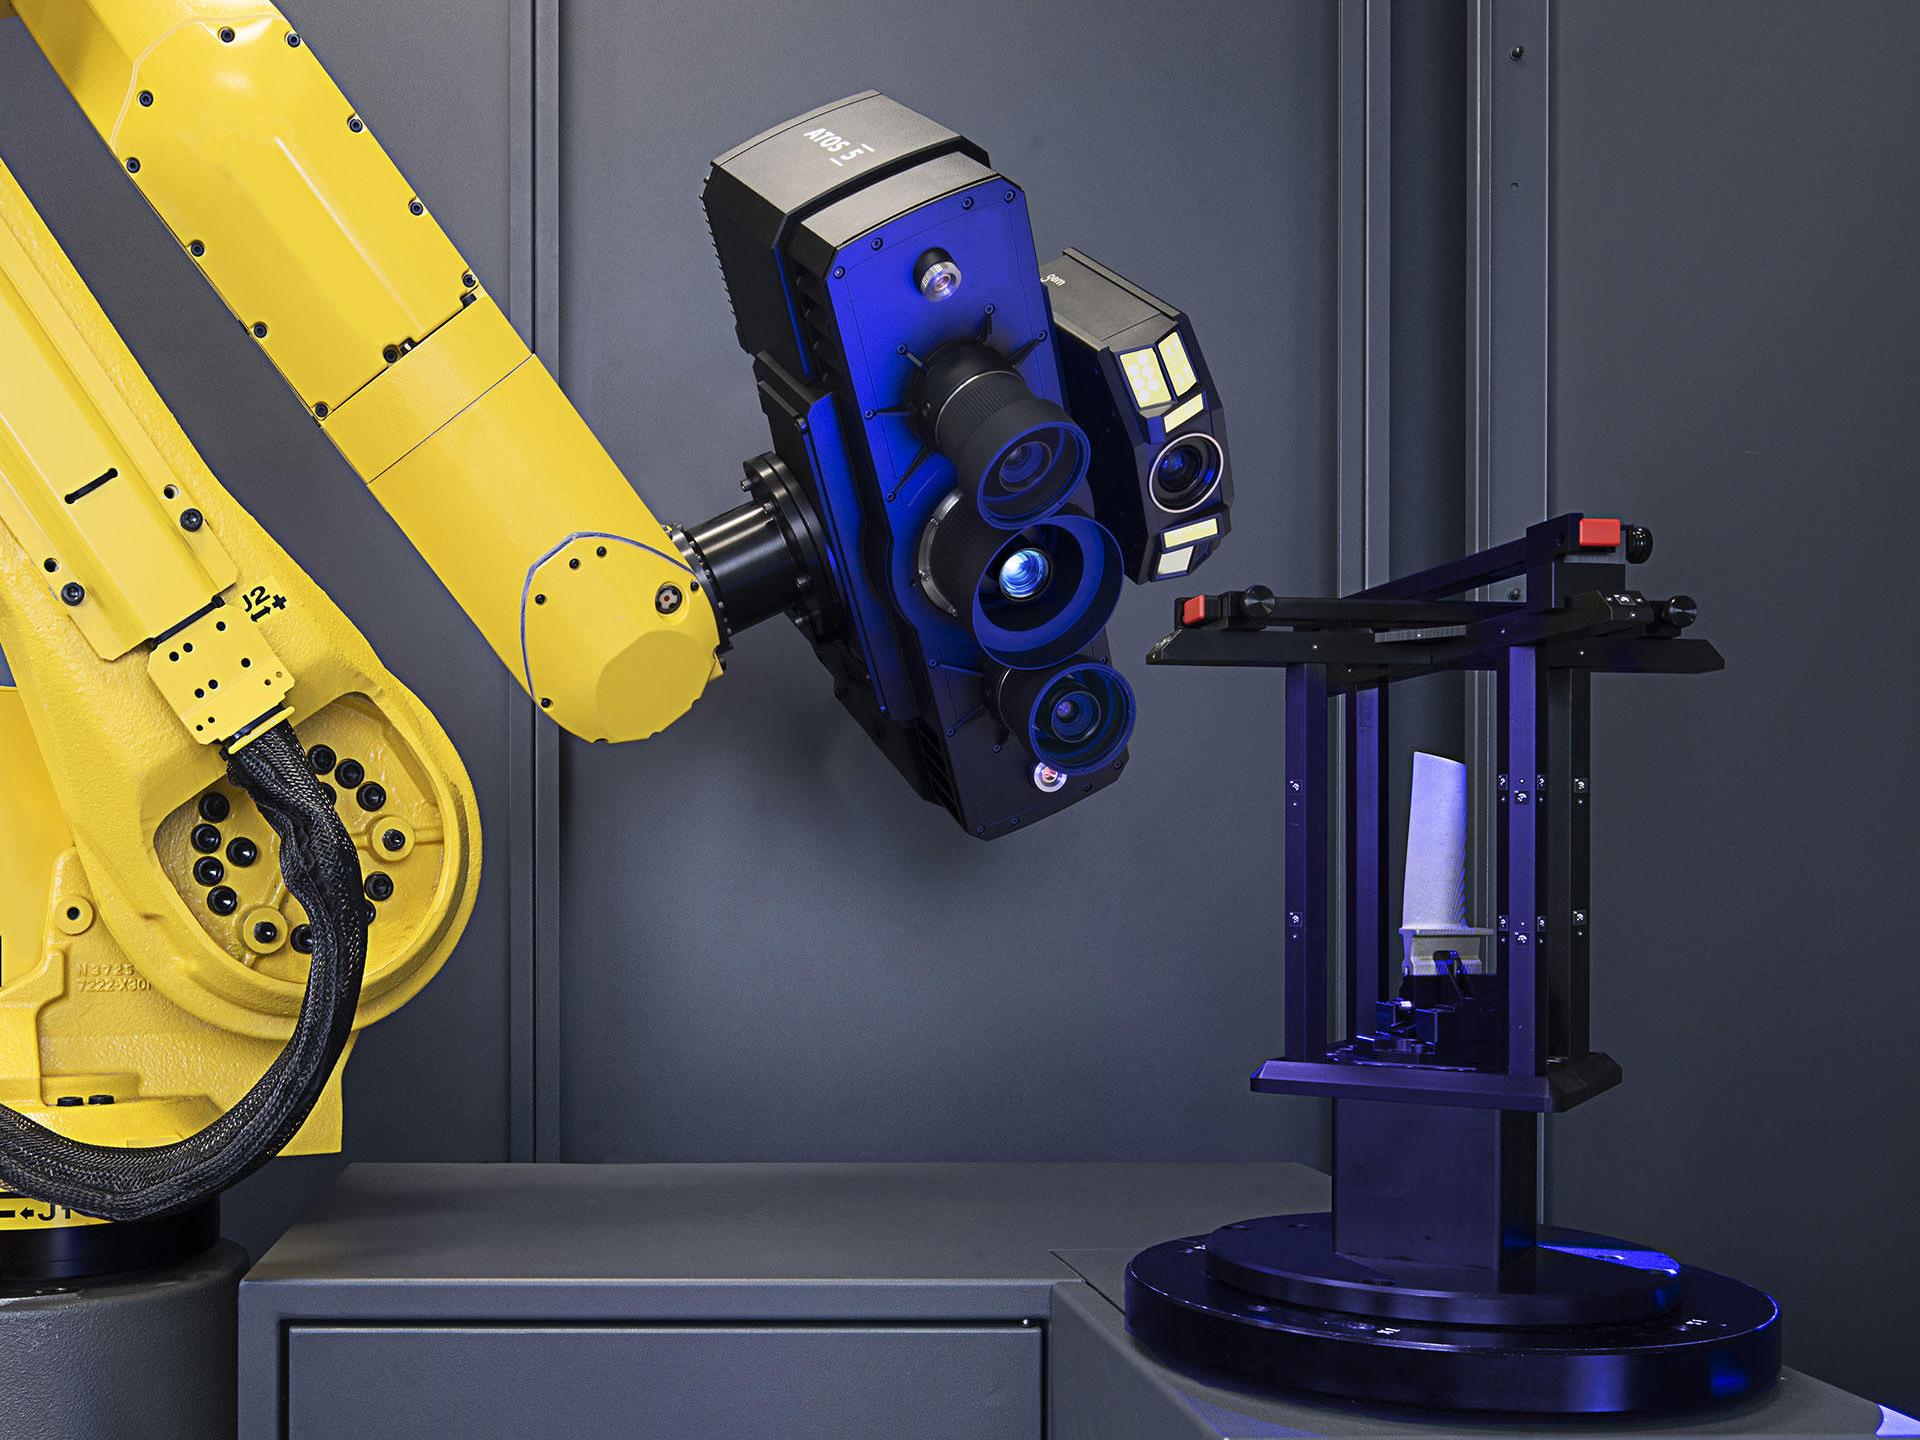
ATOS Q for full-field surface measurement
The ZEISS ATOS Q is an industrial 3D scanning system designed for full-field surface measurement. Its optical approach makes it relevant when the inspection requirement centres on complex external geometry rather than a limited set of discrete points.
For turbine blade work, this type of measurement can support dimensional verification, part-to-CAD comparison, first article inspection and analysis of freeform surfaces.
GOM Scan 1 for compact 3D inspection workflows
The ZEISS GOM Scan 1 provides a compact optical 3D scanning approach for detailed component inspection. It can be relevant where the component and inspection workflow suit a smaller, mobile scanning setup.
For a broader explanation of how industrial 3D scanners differ by measurement method, workflow and application, see our guide on choosing an industrial 3D scanner in Singapore .
The Root Attachment: Why CMM Measurement Matters
The blade root performs a very different function from the aerofoil. It connects the blade to the turbine disc and contains precisely defined features that control how the blade fits and is positioned.
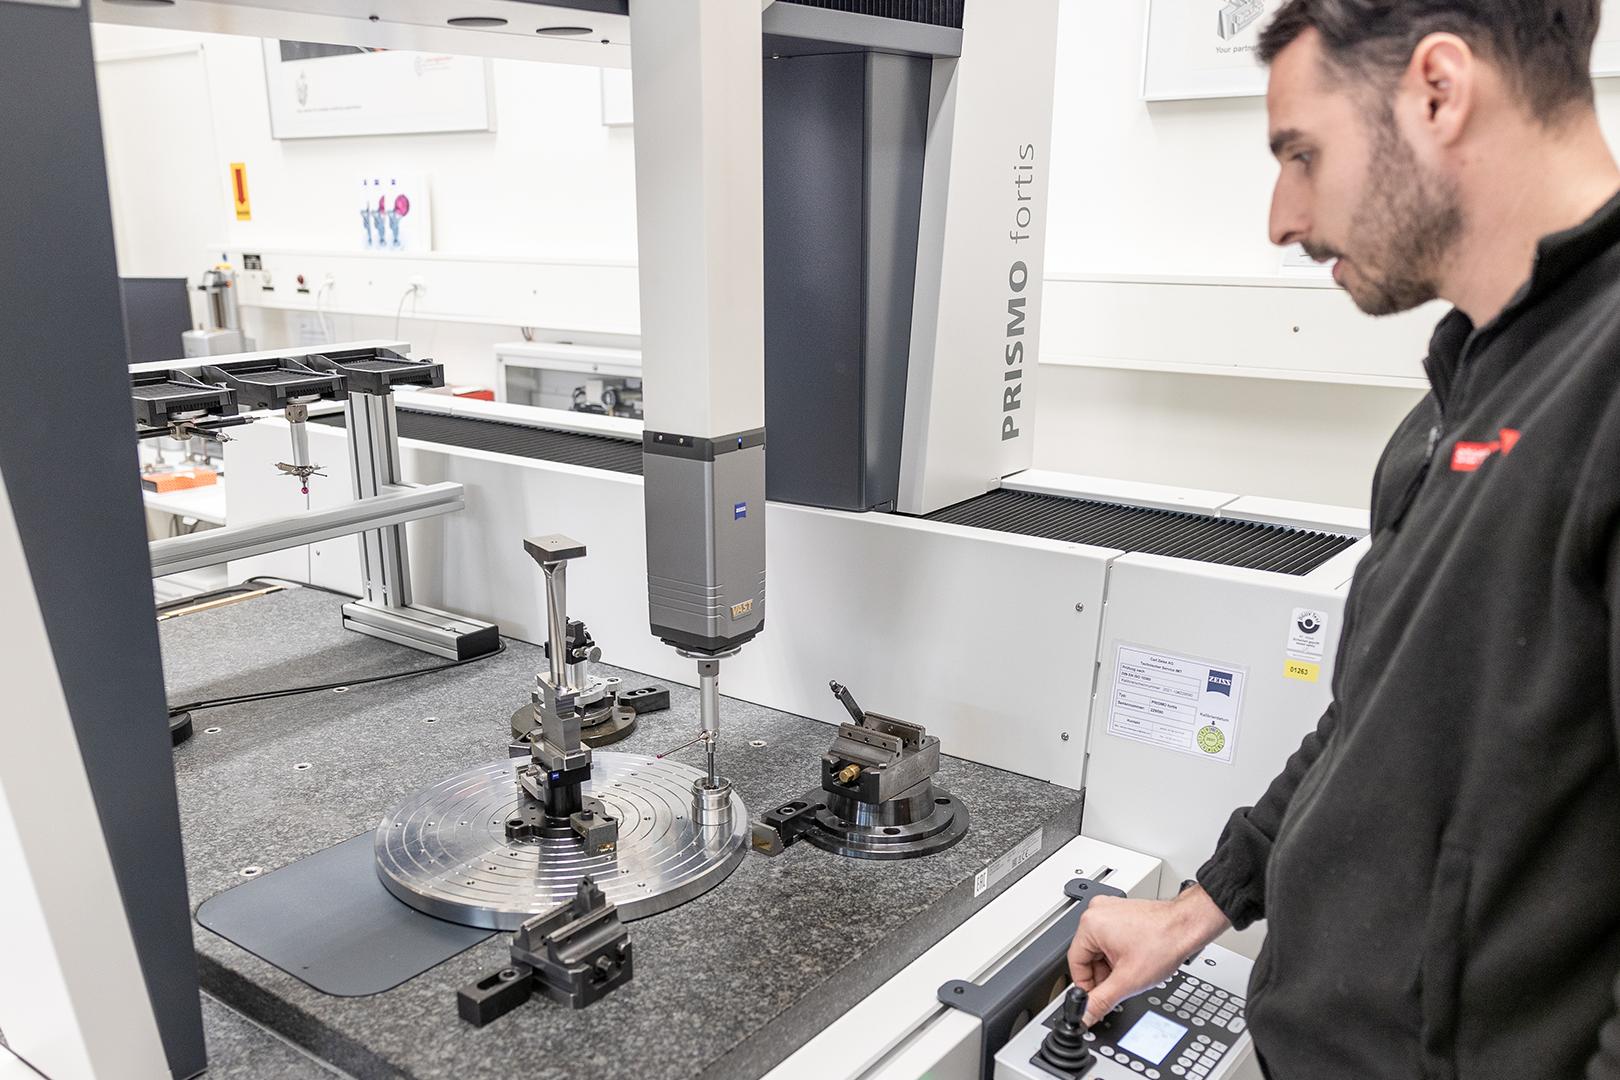
This geometry is better suited to a measurement strategy built around defined features, datums and geometric tolerances. A coordinate measuring machine can probe critical surfaces and calculate dimensions and geometric relationships against the engineering requirements.
The important measurement is therefore not simply whether one individual dimension is within tolerance. The relationship between features matters as well. Datum structure, profile, position and orientation all form part of understanding whether the attachment geometry corresponds to the intended design.
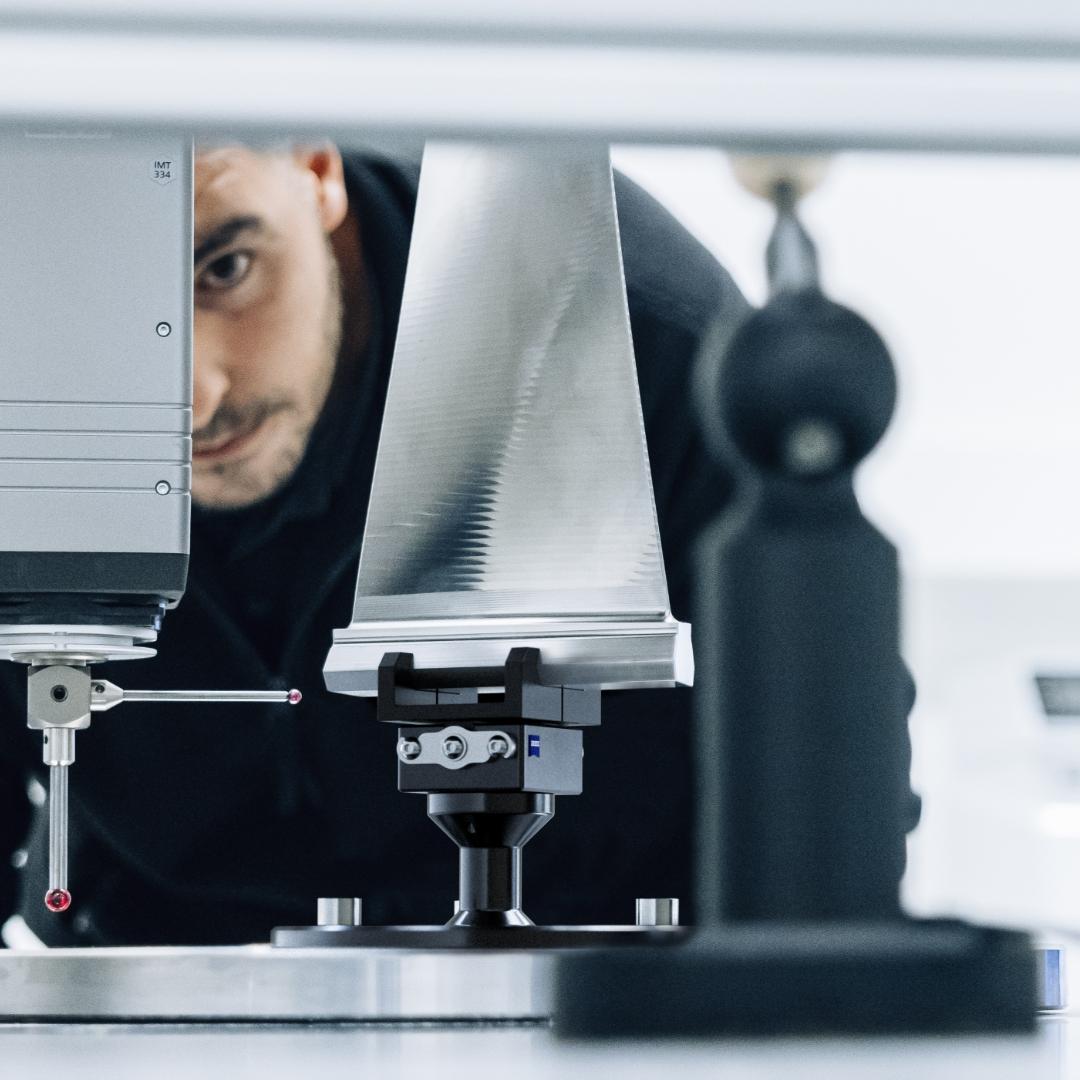
ZEISS SPECTRUM for dimensional inspection
The ZEISS SPECTRUM family provides a bridge-type CMM platform for high-accuracy dimensional measurement. It can support inspection workflows where the engineering requirement is centred on defined features, tolerances and dimensional relationships.
CMM measurement is about relationships, not isolated numbers
A turbine blade root may contain multiple surfaces and features that work together during assembly. Measuring each feature independently without considering its datum structure can provide an incomplete picture.
This is where CMM inspection becomes particularly useful: the measurement process can be structured around the engineering definition of the component rather than simply collecting arbitrary points.
The Internal Cooling Passages: Where CT Becomes Essential
The internal cooling passages are one of the clearest examples of why turbine blade inspection cannot rely on one measurement method.
Cooling channels are embedded inside the blade structure. Their geometry can be critical to the component, but external measurement cannot provide direct access to the entire internal structure.
Industrial X-ray computed tomography, or CT, provides a non-destructive way to visualise internal geometry. The resulting volumetric data can be used to investigate internal channels, wall thickness, cavities and other features that cannot be reached using conventional external measurement.

Internal geometry, wall thickness and defects
CT data can be used to inspect more than whether a cooling passage exists. Depending on the application, engineers can analyse internal dimensions, wall thickness and deviations from nominal geometry.
The same volumetric dataset can also reveal internal discontinuities or defects that would not be visible from the outside of the blade.
ZEISS METROTOM 1
The ZEISS METROTOM 1 provides industrial computed tomography for non-destructive inspection and internal dimensional measurement. It is part of the current GTS ZEISS CT portfolio and provides an option for applications where internal geometry needs to be inspected without sectioning the component.
Turbine Blade Metrology for MRO and Worn Components
New turbine blades are normally measured against a known engineering definition. MRO components can present a different starting point.
A blade that has completed an operating cycle may show wear, repair modifications, dimensional changes or surface damage. Older components may also have incomplete documentation, making a straightforward comparison with an original drawing more difficult.
In these situations, inspection may become part of a broader reverse engineering or repair-validation workflow. The objective is not necessarily to reproduce every characteristic of the worn part. Instead, measurement data can help establish the current physical condition and provide information for engineering assessment.
Reverse engineering when the original CAD is unavailable
Reverse engineering can combine 3D scanning, CMM measurement and CT depending on which parts of the blade need to be captured.
External freeform geometry can be captured with optical scanning, while defined mechanical features can be measured using a CMM. CT can add internal information where the component contains hidden channels or cavities.
The resulting measurement data can then form part of a controlled engineering workflow for CAD reconstruction, comparison or repair assessment.
Learn more about reverse engineering services in Singapore and how different measurement technologies can be combined to capture a physical component.
3D Scanning vs CMM vs Industrial CT for Turbine Blades
The three technologies are not interchangeable. The most appropriate method depends on the geometry being inspected and the type of measurement data required.
| Inspection requirement | 3D Scanning | CMM | Industrial CT |
|---|---|---|---|
| Complex external aerofoil | Strong fit for full-field surface capture | Possible, but point or path strategy is required | Can capture external geometry as part of a volumetric scan |
| Blade root features | Useful for surface geometry and comparison | Strong fit for defined features, datums and GD&T | Possible, depending on material and CT requirements |
| Internal cooling passages | Cannot directly capture sealed internal geometry | Cannot directly access sealed internal passages | Designed for non-destructive internal inspection |
| Surface deviation mapping | Full-field colour deviation analysis | Feature and geometric deviation analysis | Volumetric comparison can reveal internal and external deviation |
| Reverse engineering | Strong for freeform external geometry | Strong for precise engineered features | Useful when internal geometry is part of the reconstruction |
The technologies can also complement one another. A complex turbine blade does not necessarily need to be forced into a single inspection method when different areas of the component require different measurement data.
A Practical Turbine Blade Inspection Workflow
A measurement strategy should start with the engineering question rather than the equipment. Before selecting the technology, identify which areas of the blade need to be verified and what information the inspection must produce.
01. Define the inspection objective
Establish whether the objective is dimensional verification, first article inspection, repair validation, wear assessment, reverse engineering or internal inspection.
02. Identify critical geometry
Separate freeform aerofoil surfaces from defined root features and hidden internal structures.
03. Match technology to geometry
Use optical 3D scanning, CMM measurement or CT according to the geometry and measurement data required.
04. Compare measurement data
Compare measured geometry against CAD, engineering requirements or an approved reference condition where applicable.
05. Analyse deviations
Determine where geometry differs from the required condition and distinguish manufacturing variation, wear and repair-related changes where possible.
06. Document the result
Produce measurement results and inspection reports that can support quality assurance, engineering review and manufacturing decisions.
ZEISS Metrology Solutions for Turbine Blade Inspection
Global TechSolutions provides access to a range of ZEISS industrial metrology technologies in Singapore. The appropriate system depends on the blade geometry, measurement objective and required inspection workflow.
ZEISS ATOS Q
Industrial optical 3D scanning for full-field surface measurement, dimensional inspection and CAD comparison of complex external geometries.
View ATOS QZEISS T-SCAN hawk 2
A portable handheld 3D laser scanner suited to flexible inspection, difficult-to-access geometry, large components and maintenance environments.
View T-SCAN hawk 2ZEISS SPECTRUM
A bridge-type CMM for dimensional measurement, feature verification and inspection of engineered geometries and tight manufacturing tolerances.
View SPECTRUMZEISS CONTURA
A versatile CMM platform for demanding dimensional inspection tasks, with options for tactile and optical measurement.
View CONTURAZEISS METROTOM 1
Industrial CT for non-destructive inspection of internal structures, hidden geometry and internal dimensional characteristics.
View METROTOM 1ZEISS INSPECT
Inspection software supporting 3D scanning workflows, CAD comparison, dimensional analysis, deviation evaluation and reporting.
View ZEISS INSPECTTurbine Blade Metrology Across Aerospace Manufacturing and MRO
Turbine blade inspection is not limited to final quality control. Measurement can form part of several stages of the manufacturing and maintenance lifecycle.
- Tooling and mould verification before blade production
- Casting inspection for dimensional and structural verification
- Machining verification for critical blade and root geometry
- Surface inspection after finishing and coating processes
- Internal inspection of cooling passages and hidden structures
- MRO inspection for worn, repaired or legacy components
The broader ZEISS Aerospace Metrology application page covers how CMM, 3D scanning and CT technologies can be applied across aerospace manufacturing, MRO and component inspection.
How to Choose the Right Turbine Blade Measurement Method
There is no single answer for every turbine blade inspection. The right starting point is the information that needs to be obtained from the component.
Questions to Ask Before Selecting a Metrology System
- Is the critical geometry external or internal? External freeform surfaces may favour optical scanning, while hidden geometry may require CT.
- Are you measuring a freeform surface or defined features? Freeform aerofoil geometry and discrete root features can require different measurement strategies.
- Is the blade new, repaired or worn? MRO and legacy components may require additional measurement or reverse engineering work.
- Do you need surface data or volumetric data? Surface scanning captures external geometry, while CT can provide information about internal and external structures.
- What engineering requirements must be verified? Identify the relevant dimensions, GD&T requirements, profiles, datums and inspection criteria before choosing the technology.
- What output does the engineering team need? This may include dimensional results, CAD deviation maps, internal measurements, inspection reports or data for reverse engineering.
Turbine Blade Metrology Starts With the Geometry
A turbine blade combines several different measurement challenges into one component.
The aerofoil is a complex freeform surface where dense optical 3D measurement can provide useful full-field information. The root attachment contains defined engineered features where CMM measurement can provide controlled dimensional and geometric verification.
Inside the blade, cooling passages and other hidden structures require a different approach. Industrial CT provides non-destructive access to internal geometry that conventional external measurement cannot reach.
For MRO and legacy components, these technologies can also form part of a broader inspection and reverse engineering workflow.
The important question is not which measurement technology is universally best. It is which technology provides the right measurement data for the part, geometry and engineering requirement being inspected.
Explore Our Metrology Solutions
Download our portfolio to explore our ZEISS industrial metrology solutions, measurement technologies and applications for demanding manufacturing environments.
GTS Metrology Portfolio
Get an overview of our solutions, capabilities and industrial metrology applications.
Download Portfolio ↓Have a part you need to measure?
Bring us your measurement challenge. Discuss your component, tolerance requirements and inspection objectives with our metrology specialists.